

Window Sills and String Courses
Window sills and string courses run straight through the shaping station: the parameterized cross-section cuts with standard blades, and repeat orders recall the stored program.


Open Hours:8:30am-20:30pm

WhatsApp: +86 198-5901-3937
Applicable Materials
Marble, granite, limestone, travertine, sandstone, kerbstone, quartz and architectural stone
Certifications & Credentials
CE Certified · ISO 9001:2015 · Industry Standard Drafting Participant · 120+ Countries & Regions Served
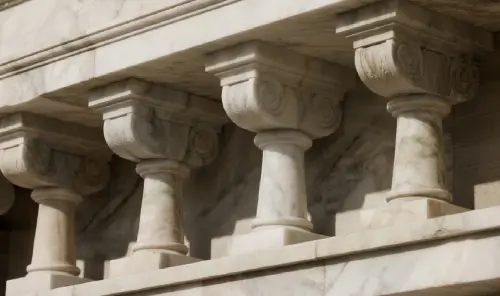
Linear molding production: window sills, door surrounds, skirting, coping, kerbstone profiles and architectural lines.
Window sills and string courses run straight through the shaping station: the parameterized cross-section cuts with standard blades, and repeat orders recall the stored program.
Door surrounds, skirting and interior moldings profile from parameter entry or DXF import — a new section is a file change, not a template remake.
Kerbstone and edging profiles cut in continuous runs on the bridge configurations, with the flatter base surface reducing manual correction after cutting.
Coping, cornices and stair nosings with anti-slip grooves profile at ±0.05 mm, ready for edge finishing without secondary profiling.
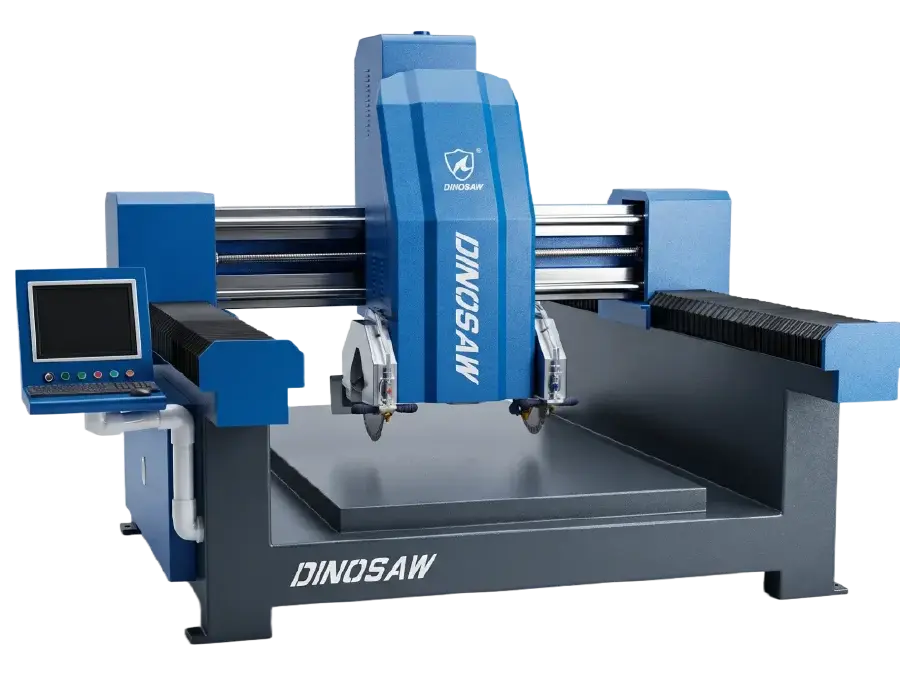
The SKFX parameter-driven stone molding machine turns profile dimensions into automatic cutting paths: the operator enters X length, Z height and R radius, the system calculates blade compensation and previews the shape in 3D, and standard saw blades cut the molding — no CNC programming, no dedicated shape tools.
Full-servo motion holds complex molding cross-sections within ±0.05 mm across repeat production — five times better than the ±0.25 mm industry standard.
Operators enter line segments, X/Z dimensions and R radii; the software generates the toolpath automatically — ordinary workers create new profiles without a CAD/CAM specialist.
Standard saw blades replace dedicated profile cutters for changing decorative line shapes, cutting tooling cost by more than 50%.
Match frame mass and spindle power to production volume, stone hardness and profile width — from compact mid-volume shops to 24-hour double-beam duty.
Applicable materials: Marble, granite, limestone, travertine, sandstone, kerbstone, engineered quartz and architectural stone.
Typical products: Door surrounds and skirting, window sills, stair nosings, coping, cornices, kerbstone profiles, Roman-column components and curved countertop edges.
Actual output varies with profile complexity, stone hardness and shift pattern.
Three SKFX configurations cover the production range: the integrated SKFX-1630/1635/1835 (3200 × 4900 × 2200 mm, 3.5 t, 15 kW, 850 mm fixed blade spacing) for versatile mid-volume shops; the single-beam bridge SKFX-3300 (7 t, 18.5 kW) for continuous single-profile runs; and the double-beam bridge SKFX-3500 (8 t, 22 kW, 2500 × 3300 mm platform, customizable 1200 mm blade spacing) for 24-hour hard-stone duty. All cut 100–1000 mm stone thickness at ±0.05 mm with Wecon CNC / G-code control.
| Specification | Integrated SKFX-1630/1635/1835 | Bridge Single-Beam SKFX-3300 | Bridge Double-Beam SKFX-3500 |
| Machine size (mm) | 3200×4900×2200 | 3550×4850 (highly customized) | 4500×4900 (highly customized) |
| Platform size (mm) | 1800×3200 (customizable) | — | 2500×3300 |
| Machine travel (mm) | 1100×3300×350 | 1200×3300×420 | 1200×3300×420 |
| Stone thickness (mm) | 100–1000 (feeding can be customized) | ||
| Spindle power (kW) | 15 | 18.5 | 22 |
| Blade spacing (mm) | 850 | 850 | 1200 (customizable) |
| Blade diameter (mm) | 300–600 | 300–600 | 500–800 |
| Control system / Run command | Wecon CNC · G code · AC 380V/50Hz · Machining accuracy ±0.05 mm | ||
| Machine weight (t) | 3.5 | 7 | 8 |
Four engineering decisions behind the parameter-driven profiling platform. The numbered points on the machine diagram correspond to the systems below.
A molding run follows four steps: enter the profile parameters (X / Z / R) or import a DXF section, verify the 3D preview and toolpath compensation, run the servo-traced cutting cycle, then check the base and profile against a gauge — a new shape is a parameter change, not a tool remake.
Instead of drawing every profile in CAM, the operator enters the segment dimensions — X length, Z height and R radius — and the system builds the cross-section automatically. Custom sections arrive as DXF imports, so both standard lines and client-specific profiles have a direct path to production.
The control calculates blade compensation and cutting passes automatically from the profile geometry, removing the manual tool-offset work that normally depends on an experienced CAD/CAM operator.
The generated profile and compensated toolpath are previewed in 3D before machining, allowing the operator to verify the shape on screen before the blade enters the stone — errors are caught in preview, not in the workpiece.
Complex moldings are cut with standard diamond saw blades instead of one dedicated shaped cutter per profile, reducing tooling cost by more than 50% and making small custom orders economical to accept.
Full-servo motion, linear guides and oil-immersed dust-protected transmission keep the programmed profile stable through long production runs — helical rack-and-pinion drives, 80 mm solid chrome-plated guide columns and accordion dust covers protect the motion system in dusty stone environments.
The second-generation cutting structure leaves the profile base substantially flatter after cutting, removing the heavy manual knock-off and base correction required by first-generation template profilers — the finished molding needs only light grinding instead of rework.
A workflow comparison for factories producing architectural linear profiles.
DINOSAW is a manufacturer of CNC stone processing machinery, specializing in diamond wire saw machines and CNC stone cutting equipment. With more than 20 years of R&D and manufacturing experience, DINOSAW contributes to industry standards including T/CMES 41001-2025 for CNC wire saw machines, holds 100+ technical patents, and supplies equipment and technical support to customers in 120+ countries and regions. Its manufacturing and management systems are certified to ISO 9001, ISO 14001 and ISO 45001, with CE-compliant machinery for international markets.

DINOSAW provides installation guidance, operator training, remote diagnosis and spare-parts coordination for every machine.
Integrated or bridge layout; double-beam for widest platforms.
Power class chosen per material hardness at order stage.
Blade cooling and slurry drainage.
Answers on parameter-driven programming, standard-blade economics, frame configuration and the data needed for an SKFX proposal.
No — that is the core of the SKFX design. Standard architectural lines are created by entering parameters: the operator types the segment dimensions — X length, Z height, R radius — and the system generates the cross-section, calculates blade compensation and previews the result in 3D. An ordinary workshop operator learns this workflow quickly, without CAD/CAM training. For client-specific sections that already exist as drawings, the second input path is DXF import: the file becomes the cutting program directly. So the machine serves both modes — parameter entry for fast standard work, DXF for custom profiles — without requiring a dedicated programmer on staff.
Because the control compensates the blade path automatically. A shaped profile tool cuts one fixed cross-section and must be remade for every new molding — costly to buy, slow to replace, and a storage problem for shops with many profiles. The SKFX instead traces the profile with a standard diamond saw blade across multiple compensated passes: the software calculates the path from the geometry, so one blade family covers any molding. This is where the 50%+ tooling cost saving comes from, and it also changes quoting behavior — small custom orders become economical because no dedicated tool investment is needed before accepting the job.
Frame mass and spindle power follow the production duty. The integrated single-beam SKFX-1835 (15 kW, 3.5 t) fits marble-primary, mid-volume shops with frequent profile changes — compact installation, fastest parameter switching. The single-beam bridge SKFX-3500 (18.5 kW, 7 t) fits granite mid-duty and continuous single-profile runs of 10 meters or more per shift — the extra structure damps vibration on long runs. The double-beam bridge (22 kW, 8 t) fits 24-hour three-shift operation, dense basalt, fiber-reinforced concrete and profiles wider than 850 mm — the twin-beam frame and customizable 1200 mm blade spacing cover the widest, hardest work. Profile complexity does not drive the choice: all three hold ±0.05 mm on any cross-section.
Any linear profile with a repeating cross-section along a straight run: door surrounds and skirting, window sills and string courses, stair nosings, coping and cornices, kerbstone profiles, Roman-column component grooves and curved countertop edges. Cross-section complexity — from a simple bullnose to a 12-step ogee — is handled by the parameter entry or DXF import at the same ±0.05 mm accuracy. If your product is a long, straight architectural element with a defined profile section, it belongs on this machine; rotational pieces like balusters belong on a stone lathe, and surface reliefs on an engraving machine.
Contact Dinosaw
Discuss SKFX Configuration & ApplicationAre you looking for the perfect cutting machines or processing solutions for hard and brittle materials?
Facing challenges in stone quarrying, countertop cutting, concrete and underwater pipeline cutting, stainless steel rust removal and grinding, luxury thin slab cutting, agate and gemstone cutting, graphite cutting, or even building demolition?
Leave your inquiry, and you can expect a reply within 12 hours with tailored solutions!






What materials will you be working with? *
Your Name / Company Name? *
Phone Number / Email Address? *
What specific requirements do you have?
Selection guides and related equipment for linear molding, sills and profile cutting.
Discover the right stone profiling machine for your factory. Our 2025 guide compares CNC, edge, and 3D profilers for granite, marble, and even glass applications.

Granite baluster and molding profiling case study using integrated CNC stone profiling machine, showing stable shaping accuracy for architectural railings and decorative stone profiles.

Tired of low-margin countertops? Discover how a CNC stone lathe transforms your fabrication business. Create high-profit architectural elements like columns & balusters.
The SKFX profiles linear sections while the LGFX stone lathe turns rotational pieces — the geometry boundary that decides between the two machines on every shaped-stone quotation.
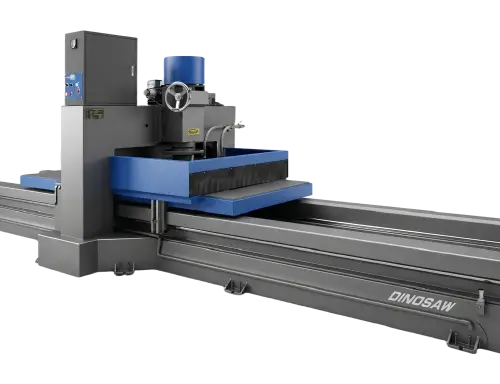
Surface detail, lettering and relief on molded elements finish on the ZDDK engraving machine — the SKFX handles the section, the engraver handles the face.
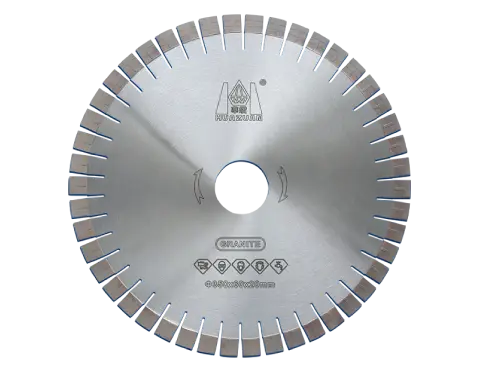
SKFX molding economics depend on standard saw blades instead of shaped cutters — the granite blade program is the tooling layer of the machine quotation.
 English
Get A Easy Solution
Chat Online
Hi, this is Lizzy from Dinosaw ( Not a Robot ). Which Machine ( model ) do you want? Please WhatsApp us now
Hello 👋 How can we help?


 中文
 Italian
 Türkçe
 Português
 Español
 Deutsch
 العربية
 Tiếng Việt
 Français
 Русский
 한국어
